Web App Development
 Cloud App Development
 Front-End Development
 Cross Platform Development
 MVP Development
 Application Modernization
 PWA Development
 SaaS Application Development
 Software Development Outsourcing
 Offshore Custom Software Development
 Full Stack Software Development
 Custom Software Development
 Enterprise Software Development
 Cloud Computing Solutions
 Cloud Development
 Managed Cloud Services
 Cloud Native Development
 AI Consulting
 Machine Learning Development
 LLM Development
 AI Chatbot Development
 Data Analytics
 CI CD Development
 Digital Transformation
 Dev Ops
 Content Development
 Blockchain Development
 Web Development
 Web Design
 Cloud Computing Solutions
 AI & ML Development
 Data Science Solutions
 UI/UX Design
 QA and Testing


 Full Stack Developers
 KnockoutJS Developers
 Microsoft Developers
 Swift Developers
 Xamarin Developers
 Blockchain Developers
 WebFlow Developers
 Software Developers
 Fintech Developers
 Security Testing Developers
 Functional Testing Developers
 Azure Developers
 Current Opening
 biz.encodedots
 biz@encodedots.com
 +91 99747 42772


- Why Traditional Manufacturing Operations Slow Down
- What Digital Transformation Actually Means on the Factory Floor
- Core IT Solutions for Manufacturing and When You Need Each
- A Step-by-Step Roadmap for Implementation
- Illustrative Scenario: Replacing Spreadsheet-Based Production Tracking
- Business Benefits and How to Measure Them
- Why Many Manufacturing Digital Transformation Projects Fail
- Don’t Overlook OT Cybersecurity
- How EncodeDots Can Help
- Frequently Asked Questions
Most manufacturers don’t need a “smart factory” overhaul. They need to fix a few specific problems: production data trapped in spreadsheets, machines that only get attention after they break, and systems (ERP, MES, quality, maintenance) that don’t share information.
The most reliable fix is a staged approach. First, find the bottleneck that costs you the most. Then connect the data behind it. Automate one high-impact workflow. Add AI only where your data is reliable enough to support it.
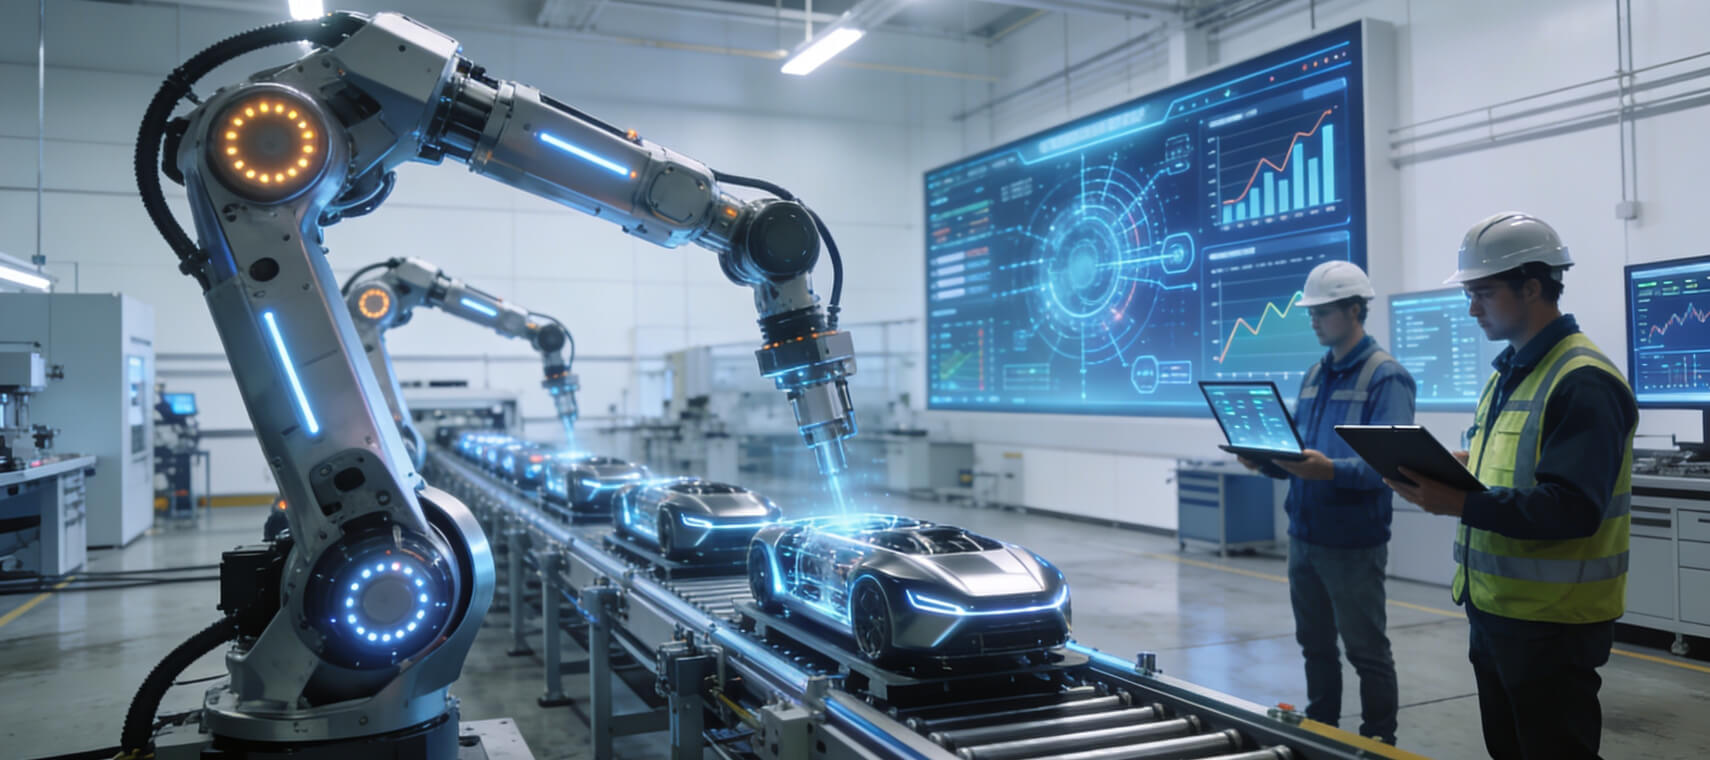
Done this way, IT solutions for manufacturing can reduce unplanned downtime, cut manual reporting, and give supervisors live visibility instead of yesterday’s numbers. This guide explains why traditional setups stall, which technologies matter, how to implement them step by step, and the mistakes that cause most projects to fail.
Why Traditional Manufacturing Operations Slow Down
Most plants don’t fail loudly. They slow down quietly. Orders ship and machines run, but inefficiencies accumulate underneath:
- Manual approvals: A simple production change moves through emails and sign-offs, taking hours instead of minutes.
- Spreadsheet reporting: Teams make decisions on data that is already a shift or a day old.
- Departmental silos: Production, maintenance, quality, and procurement keep separate records, so people duplicate work or act on conflicting numbers.
- Reactive maintenance: Equipment is repaired only after it fails, stopping the line and disrupting delivery commitments.
Together, these create an execution gap: the business plans for speed and scale, but its systems cannot deliver it.
The root cause is rarely a lack of software. It is usually disconnected data. Machines, ERP, maintenance logs, and quality records each hold part of the picture, and nobody can see all of it at once.
What Digital Transformation Actually Means on the Factory Floor
“Digital transformation” is used so loosely that it has lost meaning. Inside a plant, it is more useful to think in layers, where each layer depends on the one below it:
| Layer | What it means | Example |
| 1. Connected equipment | Machines, sensors and controllers report their status in real time | Spindle load and cycle counts streamed from CNC machines |
| 2. Real-time visibility | Data is presented in a form people can act on | A shift dashboard showing OEE by line |
| 3. Data-driven decisions | Analytics or AI recommend actions | Alerts when vibration trends suggest bearing wear |
| 4. Automated responses | Systems act within defined rules | Automatically creating a maintenance work order |
| 5. Predictive operations | The plant anticipates problems before they occur | Scheduling adjusted around forecast equipment risk |
Most manufacturers sit between layers one and three. Each layer delivers value on its own, but skipping one usually means the next fails for lack of reliable data.
Core IT Solutions for Manufacturing and When You Need Each
Not every plant needs every technology. Match each solution to a problem.
Industrial IoT (IIoT). Sensors and gateways that capture machine data such as runtime, temperature, vibration and energy use. Start here if you can’t see what your equipment is doing without walking the floor. Focus on collecting data tied to a specific decision rather than collecting everything.
Modern ERP and system integration. ERP manages orders, inventory, purchasing, and finance. Its value multiplies when it is integrated with shop-floor and maintenance systems through APIs, so production status updates automatically instead of through re-keying. If you’re evaluating platforms, our guide on what ERP is and how it works covers the fundamentals.
Real-time dashboards and analytics. Dashboards turn raw data into metrics people use, such as OEE (overall equipment effectiveness, which combines availability, performance, and quality), scrap rate, and on-time delivery. This is often the fastest visible win.
Predictive maintenance. Analytics or machine learning models flag early signs of failure from sensor trends. It works best on critical assets with consistent historical data. It is not a good first project if you have no sensor data yet.
Cloud platforms. Cloud infrastructure lets multi-site manufacturers centralize data and scale analytics without large on-site servers, while time-critical control stays on local (edge) systems.
Digital twins. A digital twin is a virtual model of a machine, line, or process used to test changes before applying them on the floor. It usually comes later, once data is mature.
Custom manufacturing apps. When off-the-shelf tools don’t fit your workflow, purpose-built web or mobile apps can handle tasks such as digital work instructions, quality checklists, or shop-floor data capture.
OT cybersecurity. Every connected device is a potential entry point. Security must be designed in from the start, not added later (covered in more detail below).
A Step-by-Step Roadmap for Implementation
Step 1: Audit your real bottlenecks
Identify what actually slows production or raises costs. Talk to operators, planners, and maintenance staff, not just management.
- How: Map one key process end to end, such as order-to-shipment, and note every manual handoff, re-keyed entry, and wait time.
- Avoid: Starting with a technology you’ve already chosen and then searching for a problem it can solve.
- Success signal: A ranked list of three to five problems with an estimated cost or time impact for each.
Step 2: Build a unified data foundation
Decide which system is the “source of truth” for each type of data (orders, inventory, machine status, quality results) and connect them.
- How: Use APIs or integration middleware to link ERP, MES, maintenance, and quality systems. Standardize part numbers, machine IDs, and units of measure.
- Avoid: Building dashboards on inconsistent data. A good-looking chart built on bad data damages trust quickly.
- Success signal: The same figure, such as today’s output, matches across every system and report.
Step 3: Automate one high-impact workflow
Pick a workflow with heavy manual effort and measurable output, such as production reporting, work-order creation or quality inspection records.
- How: Start with existing tools and integrations before commissioning custom development. Build custom software only when off-the-shelf options can’t fit the process.
- Avoid: Automating a broken process. Simplify the workflow first, then automate it.
- Success signal: Reduced processing time and fewer data-entry errors for that workflow, measured against a baseline.
Step 4: Introduce AI where the data supports it
Good first candidates are predictive maintenance on critical assets and visual defect detection, because both have clear, measurable outcomes.
- How: Run a time-boxed pilot on one line or asset group. Plan for ongoing model monitoring and retraining (MLOps), because models lose accuracy as conditions change.
- Avoid: Launching AI on sparse or unreliable data, or deploying without operator involvement.
- Success signal: The model’s alerts are accurate enough that teams act on them.
Step 5: Scale what works
Document what made the pilot succeed, including data requirements, integrations, training and ownership, and turn it into a repeatable rollout playbook for other lines or plants.
Illustrative Scenario: Replacing Spreadsheet-Based Production Tracking
The following is a hypothetical example, not an EncodeDots case study.
A mid-sized component manufacturer tracks daily output in spreadsheets that supervisors update at the end of each shift. Planners don’t see shortfalls until the next morning, and maintenance logs live in a separate system.
Following the roadmap, the company:
- Identifies late visibility of line stoppages as its costliest problem.
- Connects machine run/stop signals and ERP work orders to a shared database.
- Replaces the end-of-shift spreadsheet with a live dashboard and automatic downtime logging.
- After several months of clean data, pilots predictive maintenance on its two most critical machines.
The AI pilot is possible only because the earlier steps created reliable data.
Business Benefits and How to Measure Them
When implemented well, manufacturing IT solutions can deliver:
- Less unplanned downtime: through condition monitoring and predictive maintenance.
- Fewer manual errors: by removing re-keyed data between systems.
- Faster decisions: because supervisors see live data instead of yesterday’s reports.
- Better quality control: through consistent digital inspections and earlier defect detection.
- More productive teams: less time spent chasing information.
Results depend on your starting point, data quality, and adoption. Record a baseline before you begin, then track:
- OEE by line or asset
- Unplanned downtime hours
- Scrap and rework rate
- Time spent on manual reporting
- On-time delivery rate
Why Many Manufacturing Digital Transformation Projects Fail
Most failures come from execution, not technology:
- Digitizing broken processes: New software makes a bad workflow faster and more expensive.
- Excluding operators: Systems designed without frontline input lead to low adoption and workarounds.
- Doing too much at once, or too little: Big-bang rollouts create chaos, while endless pilots never scale.
- Ignoring integration: New tools that don’t connect to legacy systems add complexity instead of removing it.
- Choosing tools before defining the problem: A good solution applied to the wrong issue still fails.
Don’t Overlook OT Cybersecurity
Connecting machines to networks expands the attack surface, and a breach in a plant can mean stopped lines or safety incidents, not just data loss. IBM’s X-Force Threat Intelligence Index has ranked manufacturing among the most targeted industries for cyberattacks in recent years.
Practical safeguards include:
- Segmenting OT (operational technology) networks from business IT networks
- Applying least-privilege access and multi-factor authentication for remote access
- Keeping an inventory of every connected device
- Maintaining tested, offline backups and an incident response plan
NIST Special Publication 800-82 Rev. 3, Guide to Operational Technology (OT) Security, is a useful, vendor-neutral reference for building these controls.
How EncodeDots Can Help
If disconnected systems or manual processes are holding back your operations, EncodeDots can help you plan and build the right solution, from integrating your ERP and shop-floor systems to developing custom manufacturing applications, real-time dashboards, and AI-driven tools. We start with your actual workflows and recommend the simplest approach that solves the problem.
Ready to find your biggest bottleneck? Schedule a consultation with our team.